What edge lift looks like and what it is not
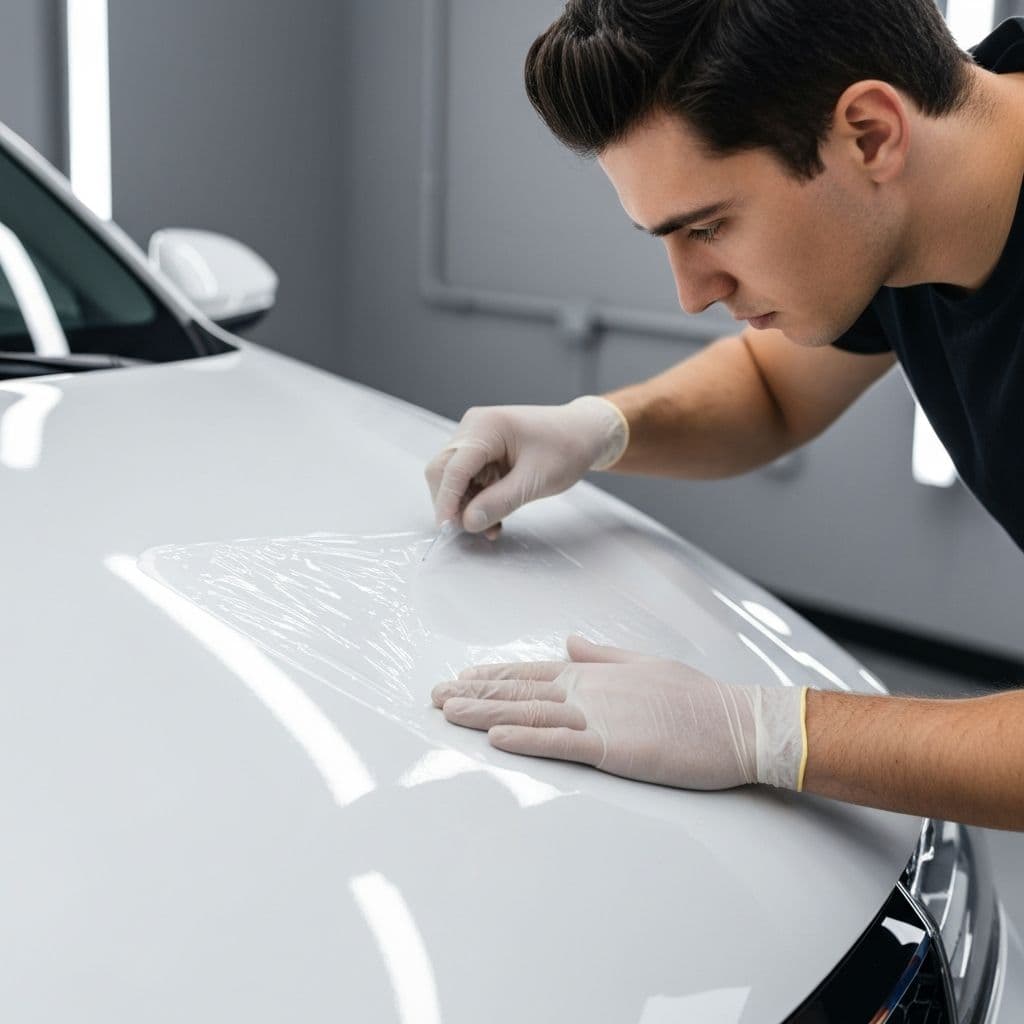
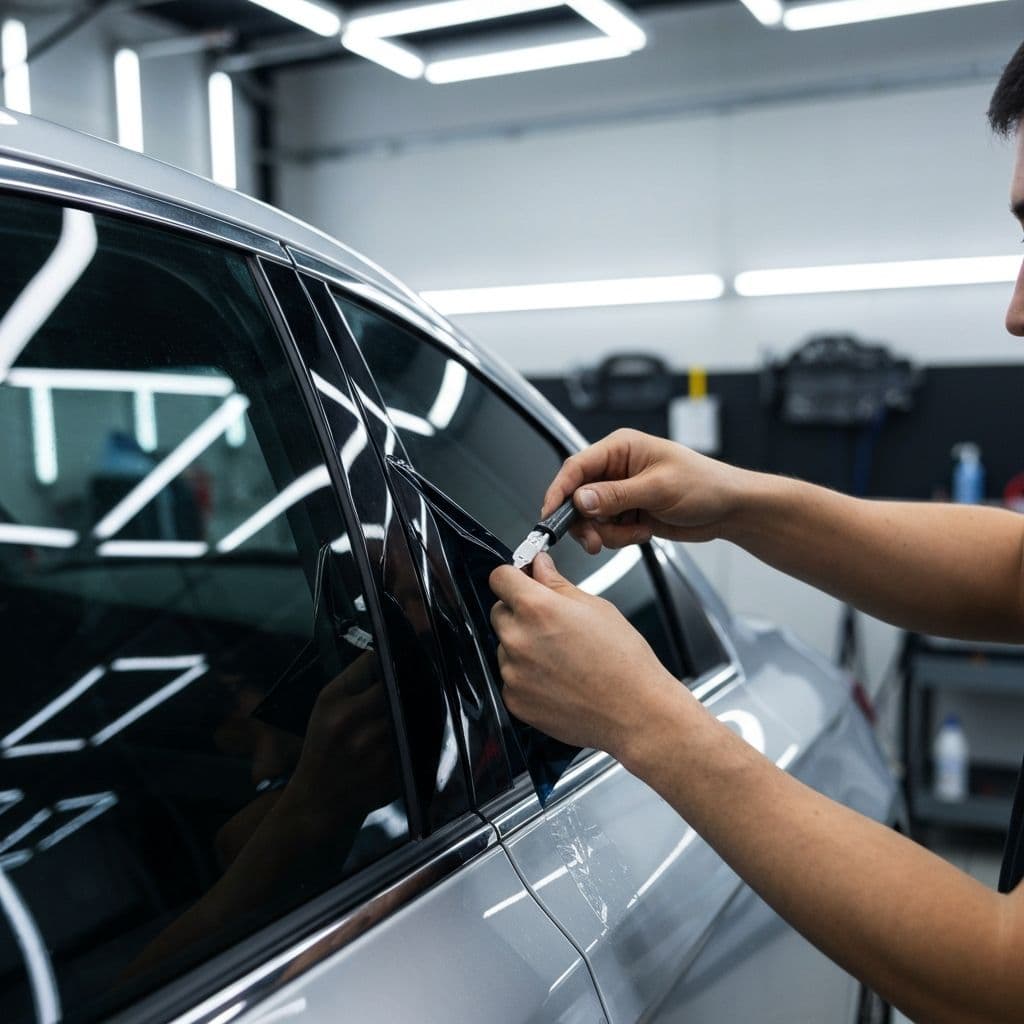
Edge lift is the failure mode where the film's perimeter stops sitting flush and begins to curl, stand proud or peel back. It may appear as a lip that catches a fingernail, a whitish line, or a section that opens after a wash or heat exposure. In wholesale PPF, the useful question is not 'is this a bad roll?' but 'where in the application and material chain did the edge lose adhesion?' PPF is a thermoplastic urethane film applied with a pressure-sensitive adhesive; edge lift can come from application conditions, surface preparation, relief/tension or adhesive/primer compatibility, not from one grade label alone.
It is not the same as an intentional wrapped edge, a field blister away from the perimeter, or impact damage. It is not proof of a batch problem. Treat it as a symptom with several possible causes and work in diagnostic order.
Start with the surface and contamination record
The edge has a narrow adhesive contact area and often sits near a seam, repaint edge, tight radius or relief cut. Start with the surface record, not the film label. Ask how the panel was cleaned and degreased, whether wax, sealant, coating or residue remained, and whether the panel had been repainted or blended. If the shop cannot reconstruct prep, record that as missing evidence rather than a film conclusion.
Contamination can be invisible: a finger mark, polishing residue or panel-wipe carrier can create a weak line exactly where the edge later lifts. The point is not to blame the installer by default; it is to establish whether the surface was controlled. If the same process gives clean edges elsewhere, this panel's history matters. If there is no prep record, the application side is unverified.
Check tension, relief and post-heating
Film stretched hard over a curve stores energy at the perimeter; when it relaxes, that energy can pull the edge. A pattern that leaves too much tension at a corner, or a cut without relief, can create a lift path even when the adhesive is sound. Ask whether the edge was wrapped, trimmed or relieved, whether the film was stretched at the edge, and whether the perimeter sat flat before post-heating.
Pressure-sensitive adhesive needs contact and wet-out. Ask how the edge was post-heated, whether heat was even along the perimeter, and whether pressure followed heat. Do not treat this as a guarantee that one heat setting fixes every edge; it is a diagnostic check. If post-heating was skipped or uneven, the edge is an application suspect until other evidence says otherwise.
Check adhesive and primer compatibility
Primer can be part of a controlled installation, but it is also a compatibility variable. Ask what primer was used, where it was applied, how it was dried, and whether it was used to chase an edge that was already lifting. Primer applied too heavily, not dried as intended, or used over an incompatible coating or residue can change adhesive behaviour at the edge.
Record the adhesive side separately from the surface side. PPF uses a pressure-sensitive adhesive, and adhesive performance is influenced by contact, pressure, temperature and substrate. If the shop changed primer, prep chemical or panel coating, that change belongs in the record. The goal is not to declare primer good or bad from one edge; it is to identify whether compatibility is an open variable.
What to photograph and record before contacting the supplier
Before cleaning, trimming or reheating the lifted edge, preserve the evidence. Photograph the panel overall, then a close-up of the lifted edge with a ruler or coin for scale if available. Include a second angle showing whether the lift is at a wrapped edge, cut edge, corner or seam. If there are multiple lift points, photograph each and mark them on a simple sketch. Do not pull the film back to inspect adhesive unless the supplier asks; that can destroy evidence.
Record install date, SKU, lot or roll identifier, installer, shop, panel history, prep steps, primer, post-heating method, tension/relief notes, and when the lift was first noticed. Note exposure since installation and whether the customer reports a wash, heat event or impact. Keep a timeline. This record separates a useful supplier conversation from a batch accusation. For distributor supplier evaluation, pair this with how distributors should evaluate supplier support; for new SKU screening, use how to test PPF before buying wholesale.
When the film or batch may be the cause
The film or batch may be the cause when application variables are controlled and the failure pattern still points to material. Look for a cluster: the same SKU or lot lifting across unrelated panels, shops or installers after documented prep, tension, relief, post-heating and primer records. A single lifted edge is weak evidence for a batch claim; a pattern with records is stronger. If the adhesive side appears unusual, or the same roll behaves differently from another roll on the same process, record it without overstating it.
Do not change the batch as the first diagnostic step. If the shop changes film before preserving the lifted edge, it loses the comparison. The supplier may need a sample of the failed area, the lot record and the installation record. The distributor's job is to hand over an evidence package, not a conclusion. If the checklist points to the film, request a sample and the SKU spec sheet before changing the next batch.
A distributor diagnostic checklist
1. Preserve the panel and photograph the lifted edge before cleaning or reheating.
2. Confirm the failure is edge lift, not a field blister, intentional wrap or impact damage.
3. Record SKU, lot/roll identifier, install date, installer, shop and panel position.
4. Reconstruct surface prep: cleaning, degreasing, coating, wax/sealant, repaint or repair history.
5. Confirm tension and relief at corners, seams and tight radii.
6. Confirm post-heating and pressure along the perimeter.
7. Record primer type, application area, drying and any process change.
8. Note install environmental conditions if recorded.
9. Check whether other panels, rolls or lots show the same pattern.
10. Separate application variables from material variables in writing.
11. Send the supplier photos, timeline, SKU/lot and open questions, not just a credit request.
12. Decide the next step only after evidence review.
If the checklist points to the film, request a sample and the SKU spec sheet before changing the next batch. For product-level questions, start with the paint protection film range and keep the diagnostic record attached to the SKU conversation.